What Is Industrial Colorimetry?
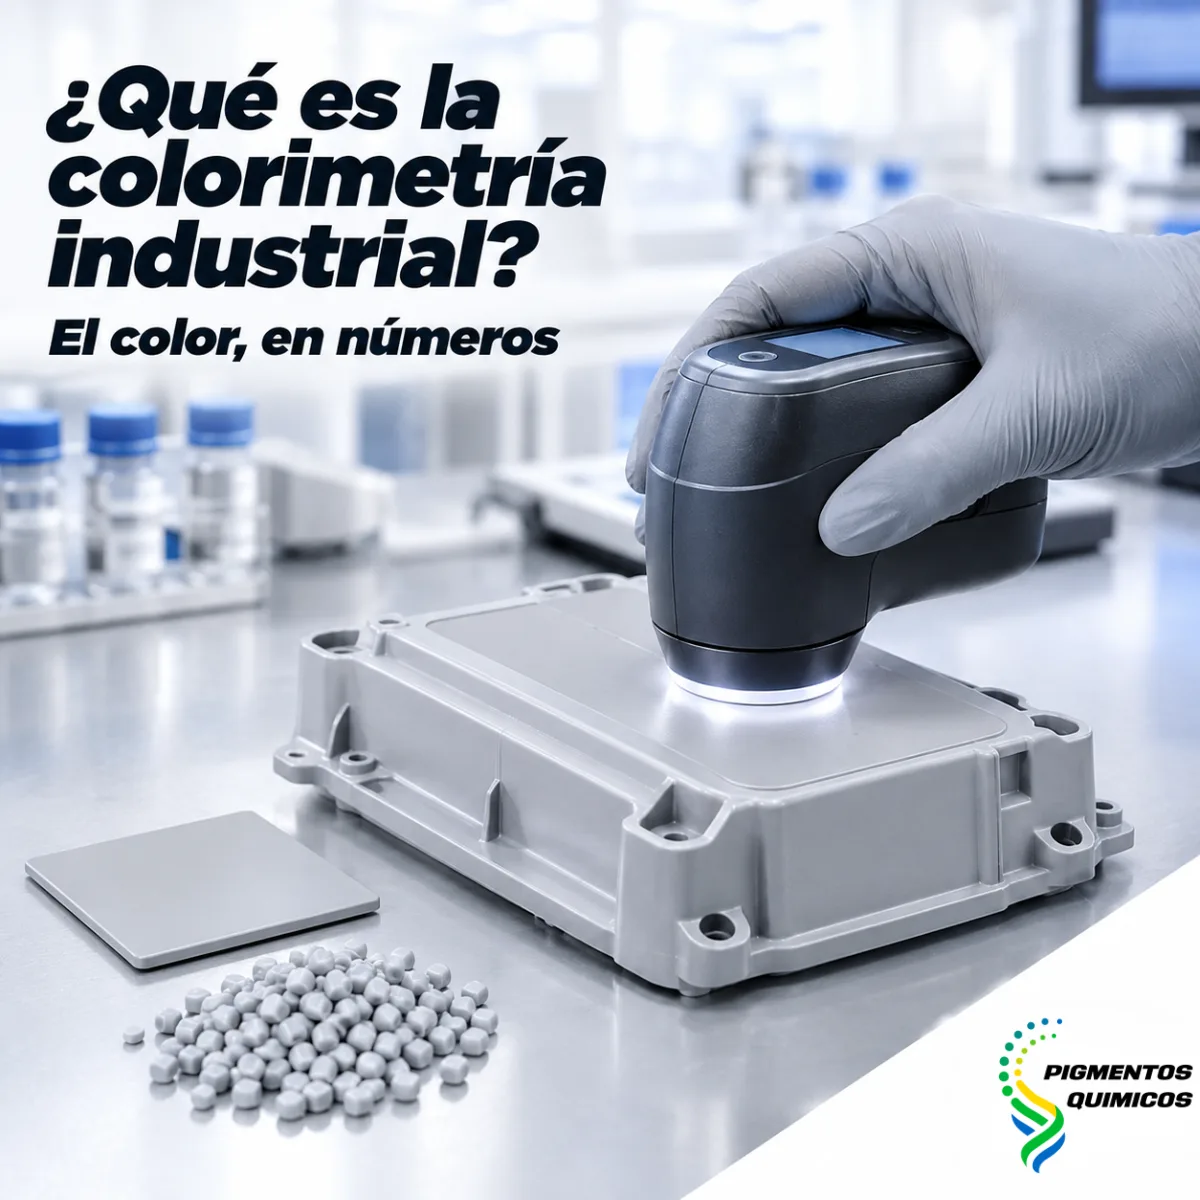
Industrial colorimetry measures color with a spectrophotometer and expresses it in CIELAB and ΔE, so every production lot is approved on objective criteria.
Your plant injection molds light gray housings for an appliance manufacturer, and the contract sets a color tolerance measured with an instrument. Your laboratory measured the first production lot, obtained a ΔE within the agreed limit and released it. A week later, the customer's quality department reported the same part as out of tolerance and held the entire shipment in its warehouse. Both measurements were correct: the customer calculated with a different ΔE formula, a different illuminant and gloss excluded, while your laboratory used the factory settings of its spectrophotometer. During the days it took to clarify which number counted, the customer's assembly line waited for parts and your finished goods inventory could not leave the plant.
Industrial colorimetry is the measurement of color with instruments under standardized conditions: light, observer, geometry and difference formula. It converts each shade into comparable CIELAB coordinates, and it only works when supplier and customer measure the same way.
From the eye to a number: what colorimetry does with the light your part reflects
A color exists thanks to three elements: a light source, an object that absorbs part of that light and reflects the rest, and an observer who interprets what is reflected. Industrial colorimetry fixes all three by standard, so that a measurement taken today at your plant can be compared with another taken next year in your customer's laboratory. In another article we explained why visual approval falls short for a contract; here we look at how the system that replaces it works.
Reflectance curve: the spectral fingerprint of each pigmentation
The spectrophotometer illuminates the sample and measures what percentage of the light it reflects at each wavelength of the visible spectrum, approximately 400 to 700 nanometers. The result is a reflectance curve, the spectral fingerprint of that pigmentation in that resin. Two parts with the same curve will look the same under any light; two parts with different curves can match under one light and separate under another. That phenomenon is metamerism, to which we have already devoted two articles, and the curve is the tool that makes it possible to anticipate it.
Illuminant and observer: the light and the eye set by the standard
To convert the curve into numbers, the calculation needs a reference light and a reference eye. The International Commission on Illumination (CIE) defines standard illuminants such as D65, which represents average daylight; A, which corresponds to the incandescent lamp; and several fluorescent illuminants, such as F2 and F11, common in offices and stores. It also defines two standard observers, 2° and 10°, according to the field of view with which the sample is observed; in color control for plastics, the 10° observer predominates. Changing any of these conditions changes the coordinates calculated for the same part.
CIELAB: the map where every color of your product has coordinates
The CIELAB space, defined by the CIE in 1976, places any color on three axes. It is the most widely used system for specifying and controlling color in plastics, because its distances approximate the differences the eye perceives and because its axes indicate in which direction to correct a lot. With it, a gray housing that someone would describe as "a little yellowish" is expressed in values that two laboratories can compare.
L*, a* and b*: lightness and two hue axes
L* measures lightness, from 0 for absolute black to 100 for ideal white. The a* axis goes from green, in negative values, to red, in positive values; the b* axis goes from blue, in negative values, to yellow, in positive values. A neutral gray part has a* and b* close to zero; if its b* rises from one lot to the next, the gray shifts toward yellow, a frequent sign of excessive process temperature or of resin degradation.
Chroma and hue angle: the reading the formulator uses
The same coordinates are also expressed in polar form, as L*C*h°. Chroma C* indicates how saturated the color is, and the hue angle h° places its hue on a wheel from 0 to 360 degrees. For the formulator, this reading is more intuitive: a lot with low chroma calls for more color strength, and a lot with a shifted hue angle calls for changing the ratio between the pigments in the formula.
Why two laboratories can measure the same part and get a different ΔE
The ΔE, or Delta E, summarizes in a single number the distance between the sample and the standard. The case of the gray housings shows that this number depends on how it is calculated and how it is measured, and that a contract that only says "maximum ΔE" leaves the door open to two valid and contradictory readings. The causes come down to three points.
ΔE formulas with different scales
The original formula, ΔE*ab, measures the straight-line distance within CIELAB. It is simple, although it treats all regions of the space equally, while the eye tolerates more chroma difference in highly saturated colors than in grays and pastels. The CMC and CIEDE2000 formulas correct that imbalance by weighting lightness, chroma and hue according to the region of the color. The same pair of parts can give very different values with each formula, so a tolerance without a declared formula has no practical meaning.
Instrument geometry: gloss included or excluded
Sphere spectrophotometers, with d/8° geometry, can measure with the specular gloss included (SCI) or excluded (SCE). The SCI reading describes the color of the material almost regardless of its finish; the SCE reading is closer to what the eye sees, because a glossy surface is perceived as darker and more saturated than a matte one of the same material. For comparing formulations, SCI is the better choice; for evaluating the appearance of parts with different textures or gloss levels, SCE. What is essential is that both parties use the same mode.
The sample: thickness, texture, temperature and background
A thin or translucent plaque lets light through, and its reading changes depending on the background it is measured on; that is why control plaques are molded at a fixed thickness with sufficient opacity, or are always measured on the same backing. Mold texture, the orientation of the part at the instrument port and temperature also shift the reading. Some pigmentations change shade while the part is still warm, so it is best to measure once it has stabilized at room temperature.
Three moments in your production where colorimetry prevents a rejection
Color matching from spectral curves
When developing a color, the formulator measures the customer's reference and looks for a pigment combination whose reflectance curve comes close to that of the standard. Computer color matching software uses databases on the behavior of each pigment in each resin to propose recipes and predict the ΔE under several illuminants. A match that reproduces the full curve of the standard holds under different lights and reduces the risk of metamerism from the very first kilogram.
Lot control: the direction of the error matters as much as its size
A ΔE outside tolerance indicates that a correction is needed; its components ΔL*, Δa* and Δb* indicate how. A positive ΔL* signals a lot lighter than the standard, which in production can come from low dosing or a thinner wall; a positive Δb* signals a yellower lot, which in a white or gray part can point to a temperature profile that is too high. With that reading, your team corrects the variable that shifted instead of raising the dosing out of habit.
Light booth: visual evaluation under controlled conditions
The instrument works alongside the trained eye. Parts with metallic or pearlescent effects, deep textures and the final appearance approval are reviewed in a booth with standard illuminants, where the sample and the standard are compared under daylight, incandescent and fluorescent light. The booth makes a visual evaluation repeatable that, on the plant floor, depends on the nearest lamp and the time of the shift.
How we use colorimetry so your color repeats in every order
Measurement conditions agreed on before production
At Pigmentos Químicos we measure color with a spectrophotometer, and we recommend putting in writing, together with the tolerance, the conditions under which it is measured: ΔE formula, illuminants, observer, gloss mode and sample type. With those five definitions in the agreement, your laboratory, your customer's and ours talk about the same number, and a lot released at your plant arrives at your customer's warehouse with the same reading.
A physical standard in your resin and your process
We develop color matches from a catalog reference or a physical sample you send us, and we formulate the masterbatch in the laboratory for your resin and your process. We send you a free one-kilogram sample so you can validate the color on your own line, and every order arrives with a quality certificate, technical data sheet and safety data sheet. The approved development, molded in your resin, is the physical standard worth keeping along with its coordinates, because plaques also age, and a reference measured in time makes it possible to replace it without losing the color.
Industrial colorimetry turns the color of your product into coordinates that any laboratory can reproduce, as long as everyone measures by the same rules. At Pigmentos Químicos we develop your masterbatch with spectrophotometric measurement and help you define the control conditions you will agree on with your customer. Tell us about your color, your resin and your tolerance at https://pigmentosquimicos.com
Frequently asked questions
What ΔE tolerance should I ask for on my product?
It depends on how visible the color is, whether the part is assembled next to others and which ΔE formula you use. A part mounted next to another from a different process or supplier calls for a tighter tolerance than a hidden component. Define it with your customer on real parts, with the formula and the measurement conditions in writing.
How often should I calibrate the spectrophotometer?
Follow the equipment manufacturer's instructions; the usual practice is to calibrate with the white tile and the black reference at the start of each shift or whenever laboratory conditions change, and to keep those references clean and protected. It is also advisable to periodically measure a control plaque of your own to detect any instrument drift.
Can the color of a transparent or translucent part be measured?
Yes, with an instrument that measures transmittance or with a fixed reflectance procedure on a constant backing. In transparent parts, color depends heavily on thickness, so the standard and the sample must have the same cross section. Agreeing on the method with your customer prevents readings that cannot be compared.