How Does the Plastic Extrusion Process Work?
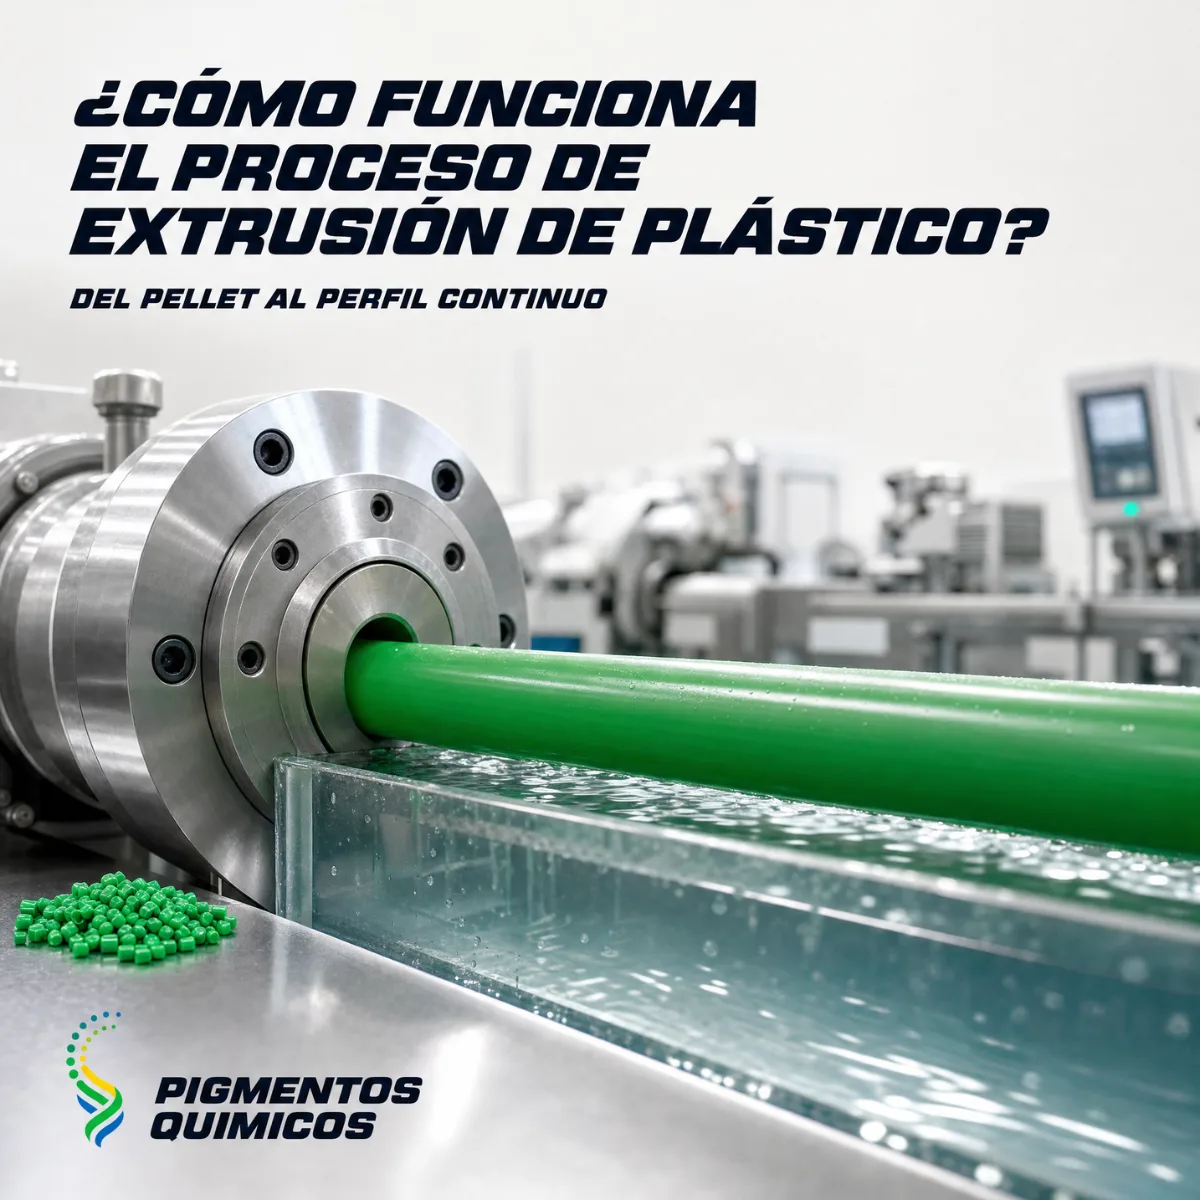
In extrusion, resin and masterbatch pass through the hopper, screw, barrel, screen and die, and are then cooled, pulled and cut or wound. Each station determines whether the color comes out uniform.
Your line of smooth orange polyethylene pipe for electrical installations ran steadily all week until, in the early morning hours, the operator changed the screen because pressure had been climbing and, to catch up on the order, increased the puller speed. For the next several hours the pipe came out a paler orange with fine streaks along its length, and nobody noticed until the morning shift compared the coils against the sample. The distributor received coils in two shades within the same order and sent back the entire shipment, because its customer in the electrical sector rejects any pipe that looks like it came from another manufacturer. The masterbatch was the same one as always; what changed was the way the line processed it.
In extrusion, resin and masterbatch pass through the hopper, screw, barrel, screen and die, and are then cooled, pulled and cut or wound. Each station determines whether the color comes out uniform.
From pellet to coil: the path where your color can be lost at every station
An extrusion line is a chain of equipment working at the same pace: the extruder melts and pushes, the die shapes, cooling sets the geometry, the puller sets the speed and the end of the line cuts or winds. If one station changes pace, the others feel it, and color is one of the first things to give it away.
Hopper and feed throat: mixing starts cold
The resin and masterbatch enter through the hopper, almost always via a feeder. If the masterbatch pellets differ greatly in size or density from the resin pellets, they separate with vibration or vacuum loading, and the ratio entering the screw changes with the hopper level. It is best to dose close to the throat and keep the material level stable. The throat is water-cooled so the pellets keep their shape until they enter the screw; if they stick together and form a bridge, throughput drops and the product shows variations in thickness and shade.
Screw: three zones with three different jobs
The screw is the heart of the process. In the feed zone, its deep flights convey the solid pellets forward. In the compression zone, the channel depth decreases, the material is pressed against the hot barrel and melts from the heat of the heater bands and from friction. In the metering zone, the channel is shallow and the already molten material is homogenized and pumped at constant pressure toward the die. Many extrusion screws also include mixing sections, with barriers or pins, that force the melt to split and recombine so the pigment is distributed better.
For color, the compression zone is the most delicate. The masterbatch carrier resin has to melt at the same time as the base resin or slightly before it, so the pigment spreads while all the material melts. If the carrier melts much earlier, it forms a lubricating layer that slips over the solid pellets without mixing; if it melts later, it reaches the metering zone in lumps the screw can no longer distribute. In both cases the result is streaks or swirls of a different shade.
Barrel and temperature profile: enough heat without punishing the pigment
The barrel is divided into independently controlled heating zones, and the temperature profile is set according to the resin, the screw and the throughput. A cold profile in the first zones delays melting and leaves unmelted material in the metering zone. One that is too hot, or a long residence time at high temperature, degrades sensitive organic pigments and the resin itself, and the shade turns brownish or loses brightness. Because much of the heat comes from screw friction, raising the screw speed raises the actual melt temperature even when the controllers show the same reading, and the shade shifts right when the line speeds up.
The screen and the die: where a dispersion defect becomes visible
Screen pack and screen changer: the filter that protects the line and also destabilizes it
Before the die, the melt passes through a screen pack supported by a breaker plate. The screens trap contaminants, gels and pigment agglomerates, and they also add resistance to flow, which raises the pressure in the screw and improves mixing. As the screen clogs, pressure rises, throughput can drop and the melt temperature changes. When the screen is changed, pressure drops suddenly and the line takes a while to stabilize; that stretch of product usually has a different thickness and a different shade.
How quickly the screen clogs is a direct indicator of the masterbatch's dispersion quality. A concentrate with agglomerates forces more frequent screen changes and multiplies the unstable transitions. Recording the pressure before the screen on every shift gives you an early warning: if it rises faster with a new lot of masterbatch, the problem is already in the material.
Die: where the cross section takes shape and streaks are born
The die distributes the melt and gives it its final cross section: a mandrel and a bushing for pipe, a profiled plate for profile, a wide lip for sheet. If the flow inside the die has zones where the material stagnates, it degrades there over time and is released as dark streaks or burnt specks. Some pigments and additives also form deposits on the die lip that leave a continuous line along the product. A clean die, with polished channels and no dead zones, matters as much for color as the masterbatch itself.
What happens after the die can also change the shade of your product
Cooling: solidification speed changes the appearance
On leaving the die, the product enters a water tank with a vacuum sizing unit, in the case of pipe and profile, or is cooled with air or over rolls, in the case of film and sheet. In semicrystalline polymers, such as polyethylene and polypropylene, the cooling rate determines how much the material crystallizes, and that crystallinity changes the opacity, the gloss and the way the color is perceived. A pipe that cools faster on one side than the other can show two shades in the same piece, and a change in water temperature between shifts can move the color of an entire production lot.
Puller: the speed that decides wall thickness and color intensity
The puller draws the product at a constant speed, and the relationship between that speed and the extruder's throughput defines the wall thickness. If the puller speeds up while the extruder holds the same throughput, the wall gets thinner; in translucent colors or those with a low pigment loading, a thinner wall looks lighter. That is what happened with the orange pipe in our example. For that reason, any change in line speed is made as a set: screw speed, puller speed and feeder rate.
Cutting and winding: the last chance to catch the defect
At the end of the line, the product is cut to length or wound into coils. This is the last point to detect a color variation before the product leaves the plant, and the right place to take control samples. Cut a sample at the start of each coil, label it with the time and lot, and compare it against the standard under the same light source. If the customer files a complaint, those samples tell you when the color changed and what was happening on the line.
How we keep your color uniform from hopper to coil
At Pigmentos Químicos we formulate extrusion masterbatch around the stations it will travel through on your line, with three decisions we make from the development stage.
A carrier that melts along with your resin and pigments suited to your temperature profile
We choose a carrier of the same polymer type as your base resin, with a melt flow suited to your extrusion grade, so it melts in the compression zone at the same pace as your resin. We select pigments with enough thermal stability for your temperature profile and for the time the material spends in the barrel, screen and die, with a margin for stoppages and slowdowns.
Controlled dispersion before the concentrate reaches your screen
We control the dispersion of the concentrate during its own manufacturing, because every agglomerate left intact in the masterbatch ends up in your screen or in your product. A well-dispersed concentrate clogs the screen less, reduces changes and keeps line pressure stable, which is the condition for uniform color throughout production.
Approval on your line with the conditions recorded
We approve the color on the product coming off your extruder and record the test conditions with your team: temperature profile, screw speed, pressure before the screen, puller speed, water temperature and dosing. With that sheet, every production lot starts from the same conditions, and any shade change can be traced back to the variable that shifted.
If the color coming off your extruder changes between shifts or after every screen change, the cause usually lies in a station on the line that stopped working at the same pace as the others. At Pigmentos Químicos we formulate the concentrate for your resin and your temperature profile, and we approve it on your own line with the conditions recorded. Tell us about your product, your resin and your extruder at https://pigmentosquimicos.com
Frequently asked questions
How often should the extruder screen be changed?
It depends on the resin, the recycled content and the dispersion quality of the masterbatch, so the best criterion is the pressure before the screen. Set a pressure limit for the change with your team and record how often it is reached. If the interval gets shorter with a new lot of material, check that lot before continuing production.
What should I do with the product made while the line stabilizes?
Separate it from conforming product and label it. Startup, screen changes and speed changes generate sections with thickness and shade out of specification. Measure the color until it holds steady against the standard, and only then resume winding the product you are going to deliver.
Does a screw with mixing sections make up for a poorly dispersed masterbatch?
It helps distribute the pigment more evenly, with a clear limit: the mixing section spreads the agglomerates throughout the melt and breaks up only some of them. The ones that survive reach the screen or the product. Fine dispersion is achieved when the masterbatch is manufactured, and the screw's job is to preserve it.