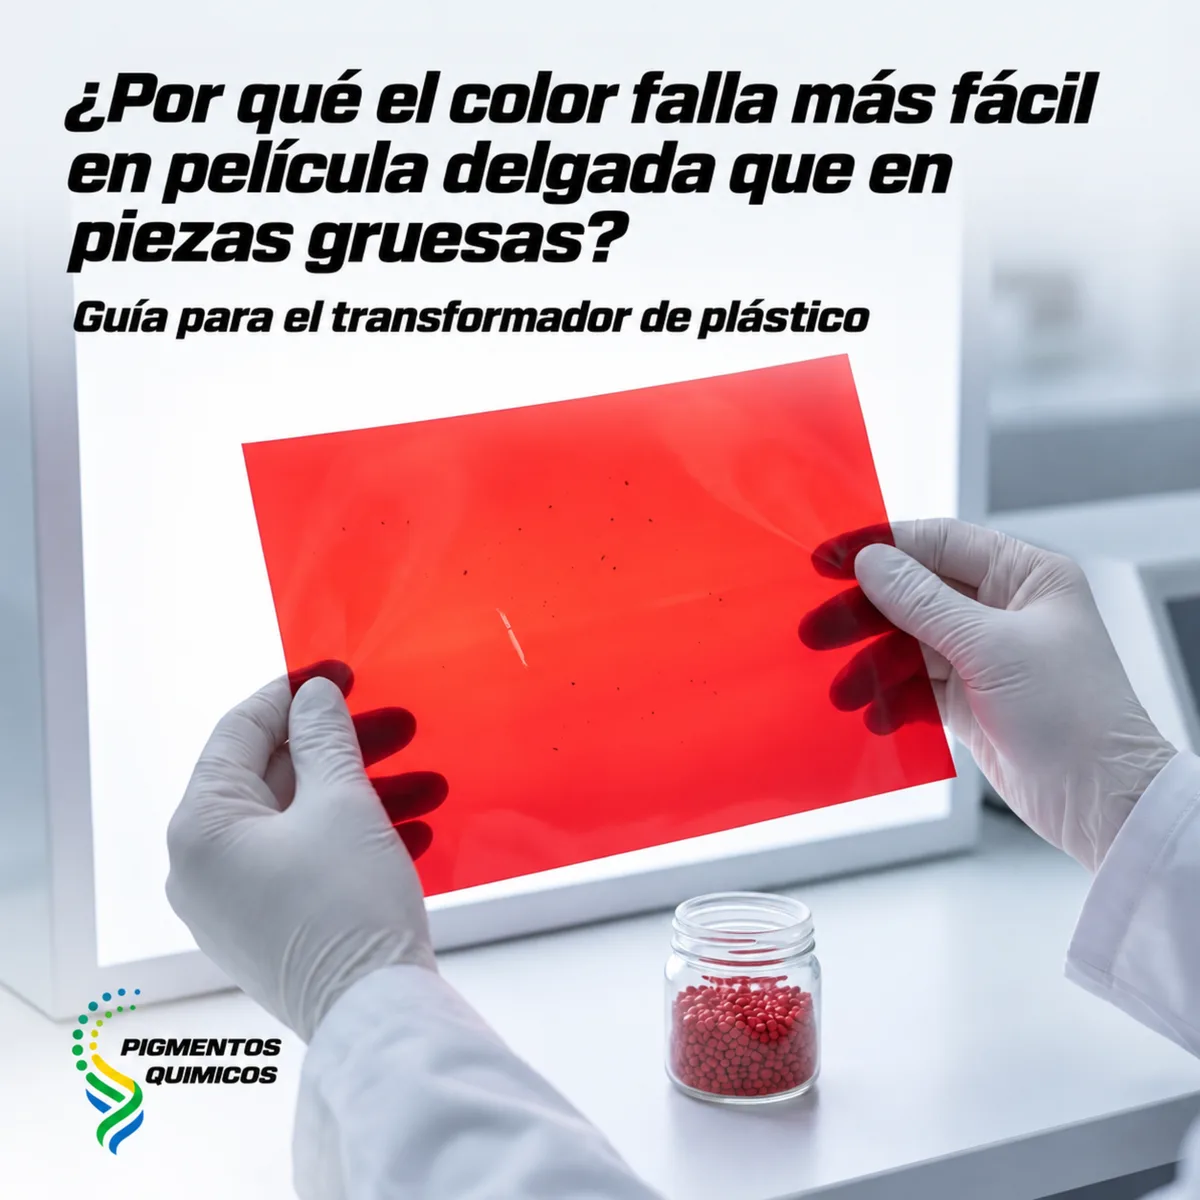
Why Does Color Fail More Easily in Thin Film Than in Thick Parts?
In a film a few microns thick, color is decided within a minimal thickness: the pigment has less path to cover, any dispersion defect is exposed and the extrusion process is harder on the concentrate. The thick part hides what the film puts on display.
The bag came off the extruder with the same masterbatch as the thick-walled crate you have been producing for years without trouble. On the crate the color is uniform; on the film there are streaks, dark specks and a shade that changes from one roll to the next. The customer returned the entire order of printed film because the background did not match their reference, and the same lot of concentrate keeps working perfectly in injection molding. Nobody at the plant understands how the same product can be right and wrong at the same time.
In a film a few microns thick, color is decided within a minimal thickness: the pigment has less path to cover, any dispersion defect is exposed and the extrusion process is harder on the concentrate. The thick part hides what the film puts on display.
Thickness decides how much color the eye sees
The color of a plastic part is the sum of the pigment that light meets on its path through the material. In a wall of two or three millimeters, that path is long and the pigment has room to absorb, reflect and cover. In a film of thirty or forty microns, the path is a hundred times shorter. The same pigment concentration produces a much weaker, more translucent color that is more sensitive to any variation.
Fewer microns, less pigment in the path of light
That is why a dosing that gives an intense blue in injection molding gives a pale blue in film, and why doubling the dosing does not always double the intensity: there comes a point where the additional pigment no longer fits well dispersed in so little thickness and starts generating defects. Color in film is designed from the thickness, with pigments of higher tinting strength and with a ratio between concentration and microns that the laboratory calculates, not that production guesses.
Why opacity is the first thing to drop
Opacity is the first thing lost. A film that would be completely opaque in the thick crate lets light through, and the product it wraps shows through. Recovering it requires opacifying pigments, typically titanium dioxide or carbon black at the right loading, and those pigments have their own dispersion demands. A film white is one of the most demanding developments there is, precisely for this reason.
Dispersion: the defect the thick wall hides
A masterbatch is never perfectly dispersed; there is always some pigment agglomerate that did not fully open. In a thick part that agglomerate is buried in the mass and cannot be seen. In a film, an agglomerate the size of the thickness itself goes through the entire wall, shows as a speck, and if it is hard, tears the film or marks the print.
Specks, streaks and fish eyes
Specks are pigment agglomerates or contaminants. Streaks are pigment that did not distribute across the width of the die and travels in a line along the roll. Fish eyes are gels or zones of unmelted resin that drag color around them. All three exist in injection molding too, invisible inside the wall; in film they are grounds for rejection, and in film for printing they also ruin the ink registration.
Carrier, melt flow index and compatibility with the film resin
The masterbatch carrier resin has to melt and blend with the film resin under the extruder's conditions. A concentrate formulated on a high-flow carrier for injection molding behaves differently in a low-flow film resin: it opens earlier or later, distributes worse and leaves zones of different intensity. That is why a masterbatch for film is formulated with the carrier and the flow of that process, and why the "same" concentrate can work on one machine and fail on another.
The film extrusion process is harder on the concentrate
Film extrusion subjects the material to conditions different from those of injection molding: temperatures specific to each resin, continuous shear in the screw, passage through filter screens and residence times that vary with line speed. Each of those variables acts on the pigment and on the carrier.
Temperature, shear and residence time
An organic pigment with a tight thermal limit can shift shade in an extrusion profile that injection molding never reaches, or degrade with a long residence time when the line slows down. Shear helps disperse, but insufficient shear in a poorly suited screw leaves agglomerates, and excessive shear degrades the resin. The same concentrate, on two different extruders, gives two results, and neither is the concentrate's fault.
Orientation and stretching change the shade
Film is stretched as it leaves the die, and in blown film it is stretched in two directions. That stretching thins the wall and orients the polymer chains, which changes how light passes through the material and how the color is perceived. A shade approved on an unoriented laboratory plaque can read differently on the roll, and the difference grows with the blow-up ratio. Color approval for film is done on film, not on a plaque.
What a masterbatch for film needs
A concentrate designed for film differs from a general-purpose one in four formulation decisions the laboratory makes from the start.
Pigments of higher tinting strength and finer dispersion
Pigments that deliver more color per gram are chosen, to reach the shade without saturating the thickness, and they are dispersed to a particle size well below the film thickness, with filtration during the manufacture of the masterbatch itself. A concentrate that passes a demanding filter test in the laboratory is the one that will not leave specks on the roll.
Carrier and process additives
The carrier is chosen with the same polymer and a flow close to that of the film resin, so both melt and blend within the same window of the extruder. In addition, a concentrate for film usually carries process additives that help disperse and keep the pigment from clustering under shear or depositing on the die. Those additives do not change the color, but they decide whether roll number one hundred comes out the same as the first or whether the line builds up deposits that end in streaks. When the film also carries slip or antiblock, the laboratory verifies that the color concentrate does not compete with them at the surface.
Dosing by thickness, not by part weight
Dosing is calculated for the target thickness, and it changes if the customer asks for a thinner film even when it is the same color. A fixed "two percent" recipe that works at forty microns gives a different shade at twenty-five. At Pigmentos Químicos we deliver the recommended dosing by thickness range, with the approval plaque made in film on your own line, so the roll matches what the customer approved.
How to approve a color for film without surprises
Approval follows four steps. The real production thickness and the exact resin are defined, including the proportion of recyclate if there is any. The concentrate is formulated for that process, with a compatible carrier and pigments of adequate tinting strength. A trial is run on your extruder, with your temperature profile and your blow-up ratio, and the roll is measured against the customer's standard. And the dosing and the conditions under which it was approved are recorded, because any change in thickness, resin or line speed moves the color again.
If the same concentrate works for you in injection molding and fails in film, the problem is that film needs a development of its own. At Pigmentos Químicos we formulate masterbatch for film with the carrier, the fineness and the dosing of your process, and we approve it on your own extruder. Tell us about your film and your thickness at https://pigmentosquimicos.com
Frequently asked questions
Can I use the same masterbatch for injection molding and for film?
Sometimes, in dark colors and with generous thicknesses. In most cases film demands a concentrate formulated for it, with a different carrier, a different dispersion fineness and a different dosing. Using the injection one tends to work until the first roll with specks.
Why does the color of the roll change with line speed?
Because speed changes residence time, stretching and final thickness. A temperature-sensitive pigment degrades more with long residence, and a slightly lower thickness lets more light through. Fixing the speed at approval and recording it avoids that variation.
What test should I ask for before approving a concentrate for film?
A filter test of the masterbatch itself, which measures how many agglomerates it leaves, and a production trial on your line with measurement of the roll against the standard. The two together anticipate the specks and the shade before committing an order.