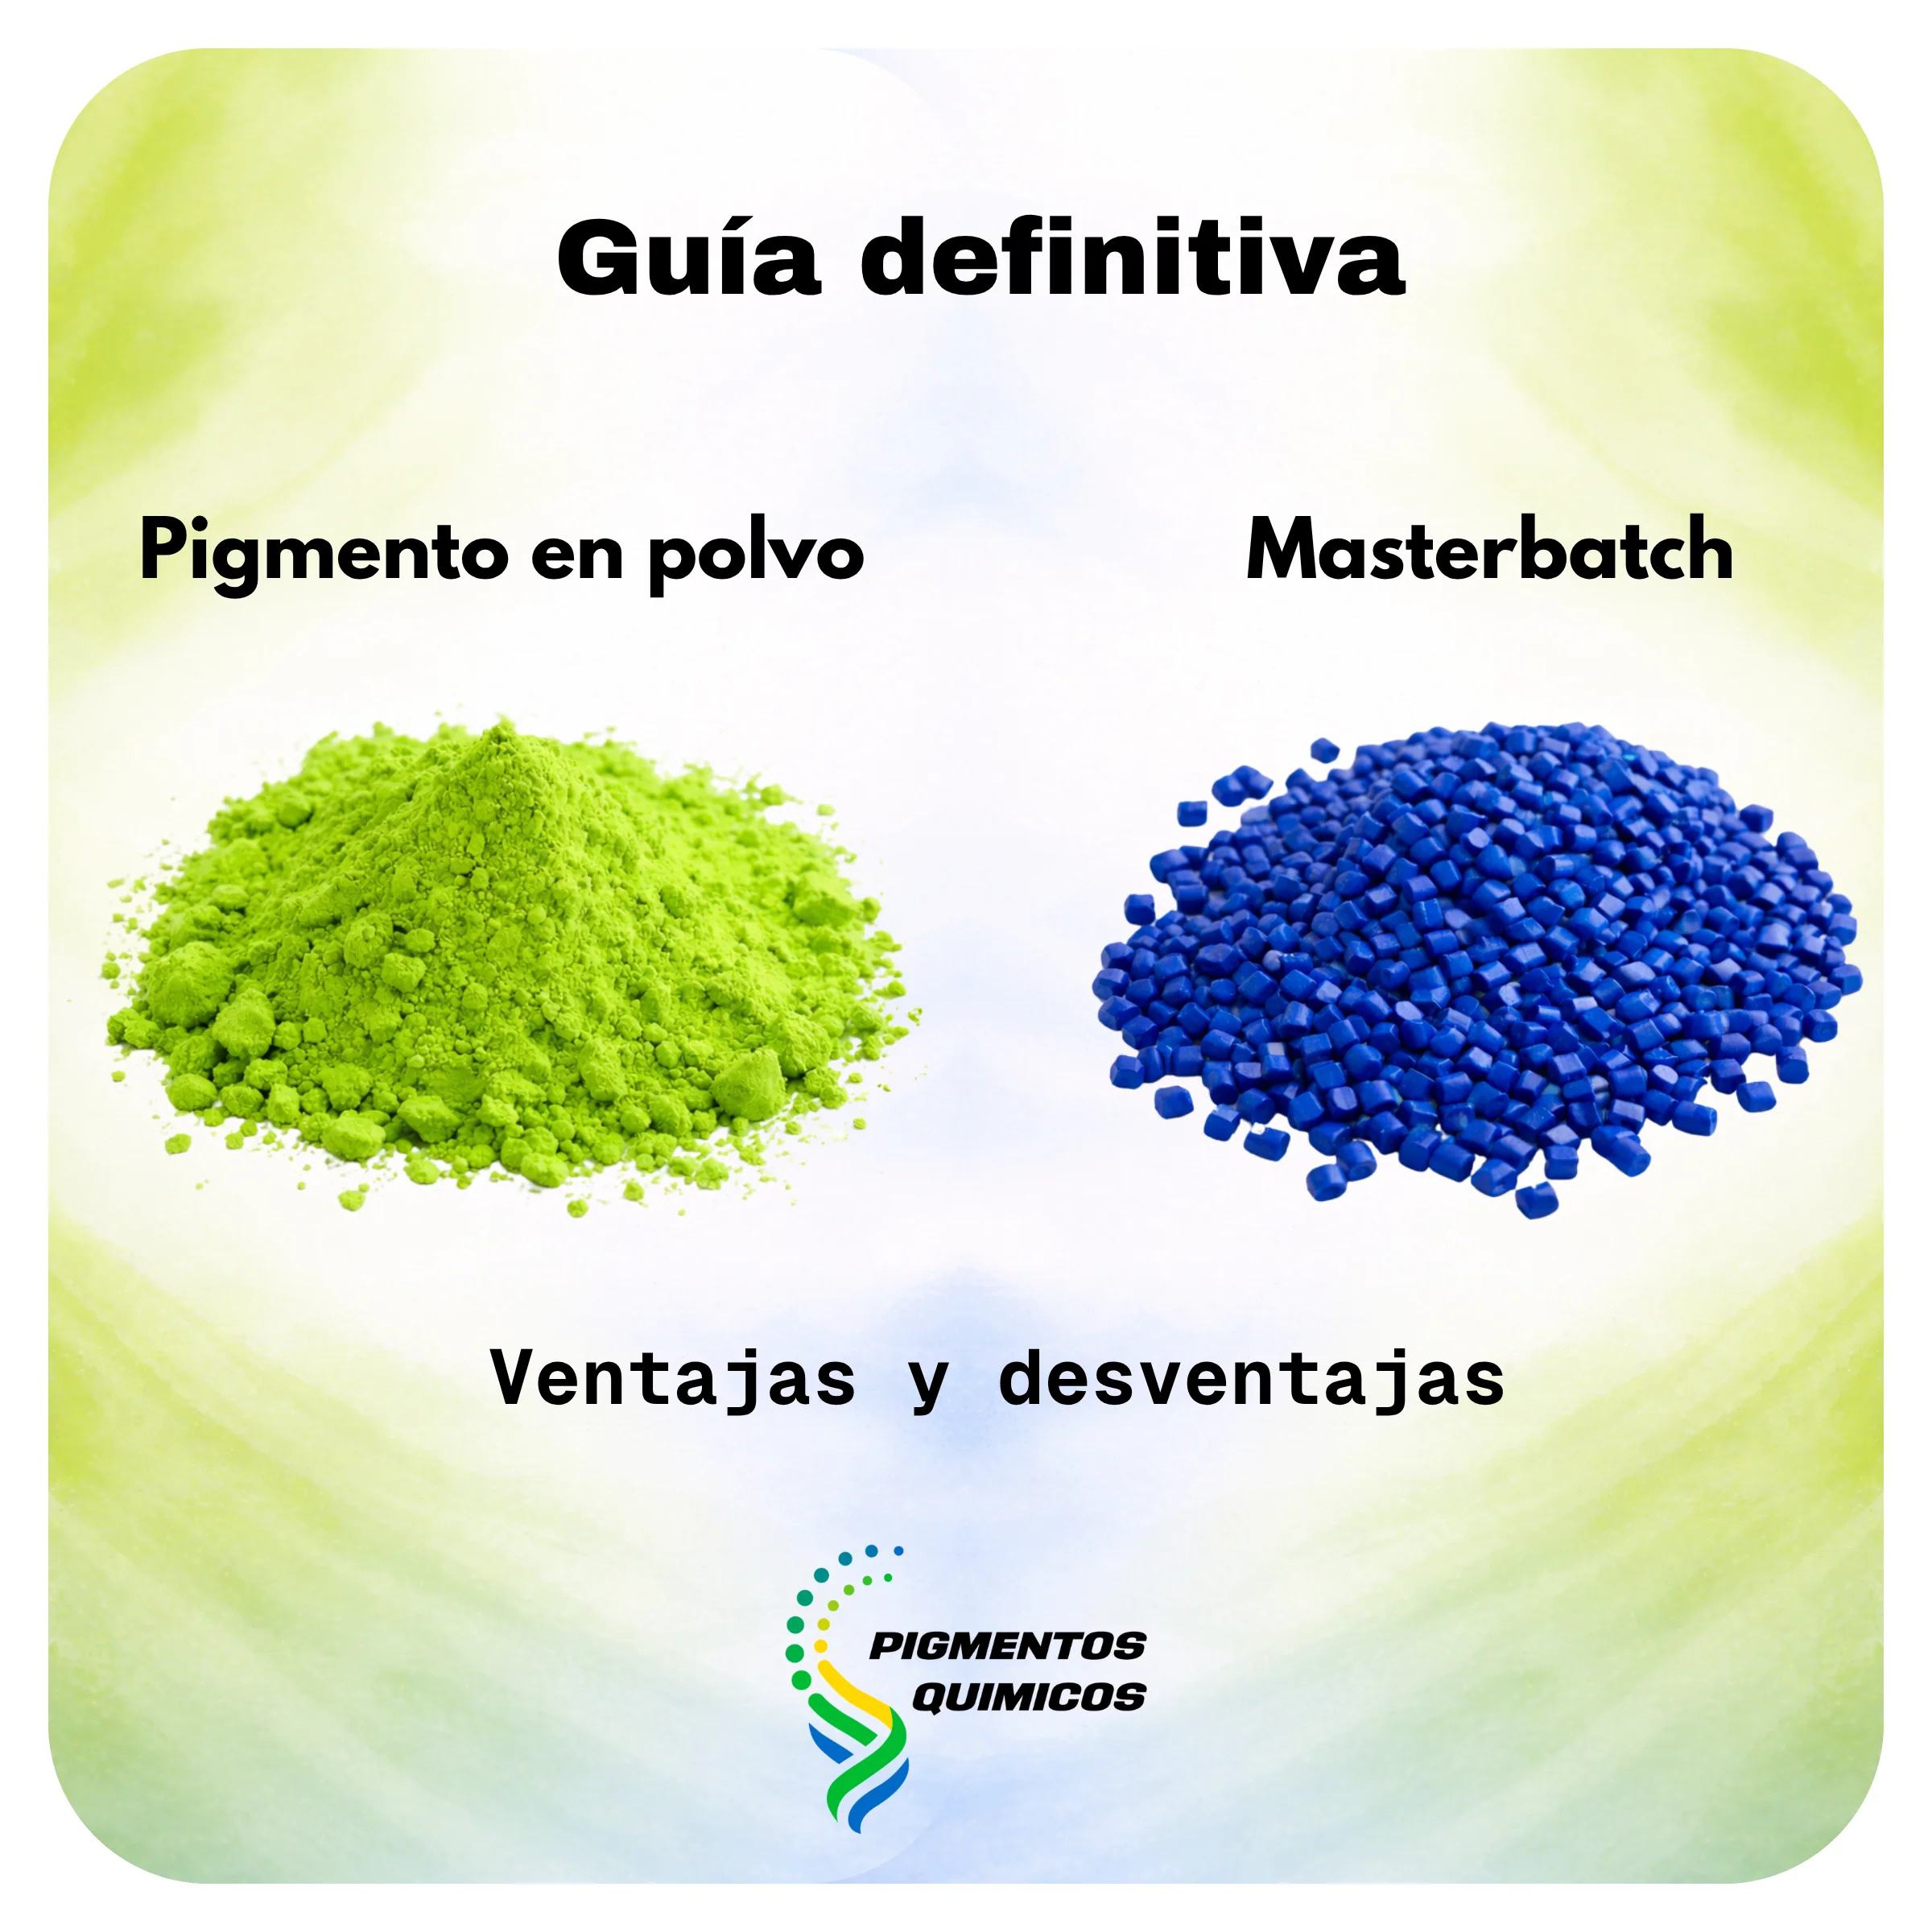
Pigment Powder vs. Masterbatch: Technical Analysis for Choosing the Right Dosing
Pigment powder and masterbatch are not interchangeable. Which scenarios make each technology pay off, technically and economically.
For process engineers and materials specialists who manage the complexity of mass coloring, the technical analysis of the transition from pure pigments to pre-dispersed systems is fundamental. Although in theory powder pigment represents the purest and most economical form of coloring, the reality on the production line reveals that the lack of a carrier vehicle compromises melt homogeneity, generates cross-contamination risks, and dramatically increases uncertainty in chromatic repeatability.
Dispersion Dynamics and Shear Energy
Using powder pigments requires the screw of the extruder or injection molding machine to perform additional mechanical work to break primary agglomerates. If the shear energy is insufficient, non-dispersed color spots are produced that act as mechanical stress concentrators in the part.
In contrast, Masterbatch has already gone through a twin-screw extrusion process, which guarantees that the pigment particles are pre-dispersed and 'wetted' by a carrier resin. This ensures immediate integration into the polymer matrix, optimizing residence time and avoiding variations in final opacity.
Industrial Hygiene and Process Stability
One of the most overlooked technical challenges of powder pigment is its volatility. Fine particles have high surface energy and tend to migrate through air currents, causing contamination in adjacent machines and safety risks for the operator.
Masterbatch, being in pellet format, eliminates airborne contamination and allows exact gravimetric dosing. This reduces human error and feeding fluctuations, which are the main cause of ΔE deviations in long production runs.
Thermodynamic Interaction and Pigment Protection
High-performance organic pigments are sensitive to direct thermal degradation. In the case of powder, the pigment comes into immediate contact with the hot barrel walls. Masterbatch acts as a thermal shield; the carrier resin encapsulates the pigment, providing a more controlled temperature transition.
For materials engineers, it is vital that the Melt Flow Index (MFI) of the Masterbatch carrier is compatible with the base resin. An MFI incompatibility will result in poor color distribution, affecting both the aesthetics and the surface tension of the finished part.
Frequently Asked Questions before making the final decision
Can I use powder pigment directly in a standard screw injection molding machine?
It is technically possible, but dispersion results are generally inferior to those obtained with masterbatch. The screw of a standard injection molding machine does not have the mixing geometry or the length to diameter ratio needed to disperse pigment agglomerates with the fineness required for applications with controlled color quality. If the application tolerates color variation and has no Delta E criteria, it can be viable. If the application requires guaranteed color consistency, masterbatch is the correct choice.
What equipment investment do I need to use powder pigment efficiently?
Using powder pigment efficiently in a standard conversion process requires, at minimum, a system to premix the powder with the resin before feeding the machine, and a gravimetric dosing system that guarantees the exact proportion of powder in the blend. For high volume production with color control, a twin screw extruder dedicated to producing the colored compound is required, which in practice means installing an in house compounding line.
Is universal masterbatch always the best option when the base polymer changes frequently?
Universal masterbatch simplifies inventory management when working with multiple polymers, but it does not guarantee the optimal color result in all of them. For applications with tight color criteria in each polymer, resin specific masterbatch always produces a better result than universal. The right choice depends on how much the color variation between polymers affects the quality of the final product: if the impact is high, specific masterbatch justifies the additional inventory.
Related articles
5 Common Problems in Plastic Coloring and How to Solve Them
The five most frequent problems in plastic coloring: poor dispersion, thermal degradation, migration, batch inconsistency, and UV discoloration.
Masterbatch vs. Liquid Pigments: Technical Analysis to Decide Correctly
Choosing between solid masterbatch and liquid pigment is not about unit price. Dosing stability, color consistency, and changeover cost decide the real cost.
Metamerism in the Plastics Industry: The Invisible Phenomenon That Ruins Production Batches
Two parts with the same masterbatch look identical under plant lighting and different under daylight. That is metamerism, and it scraps entire batches.