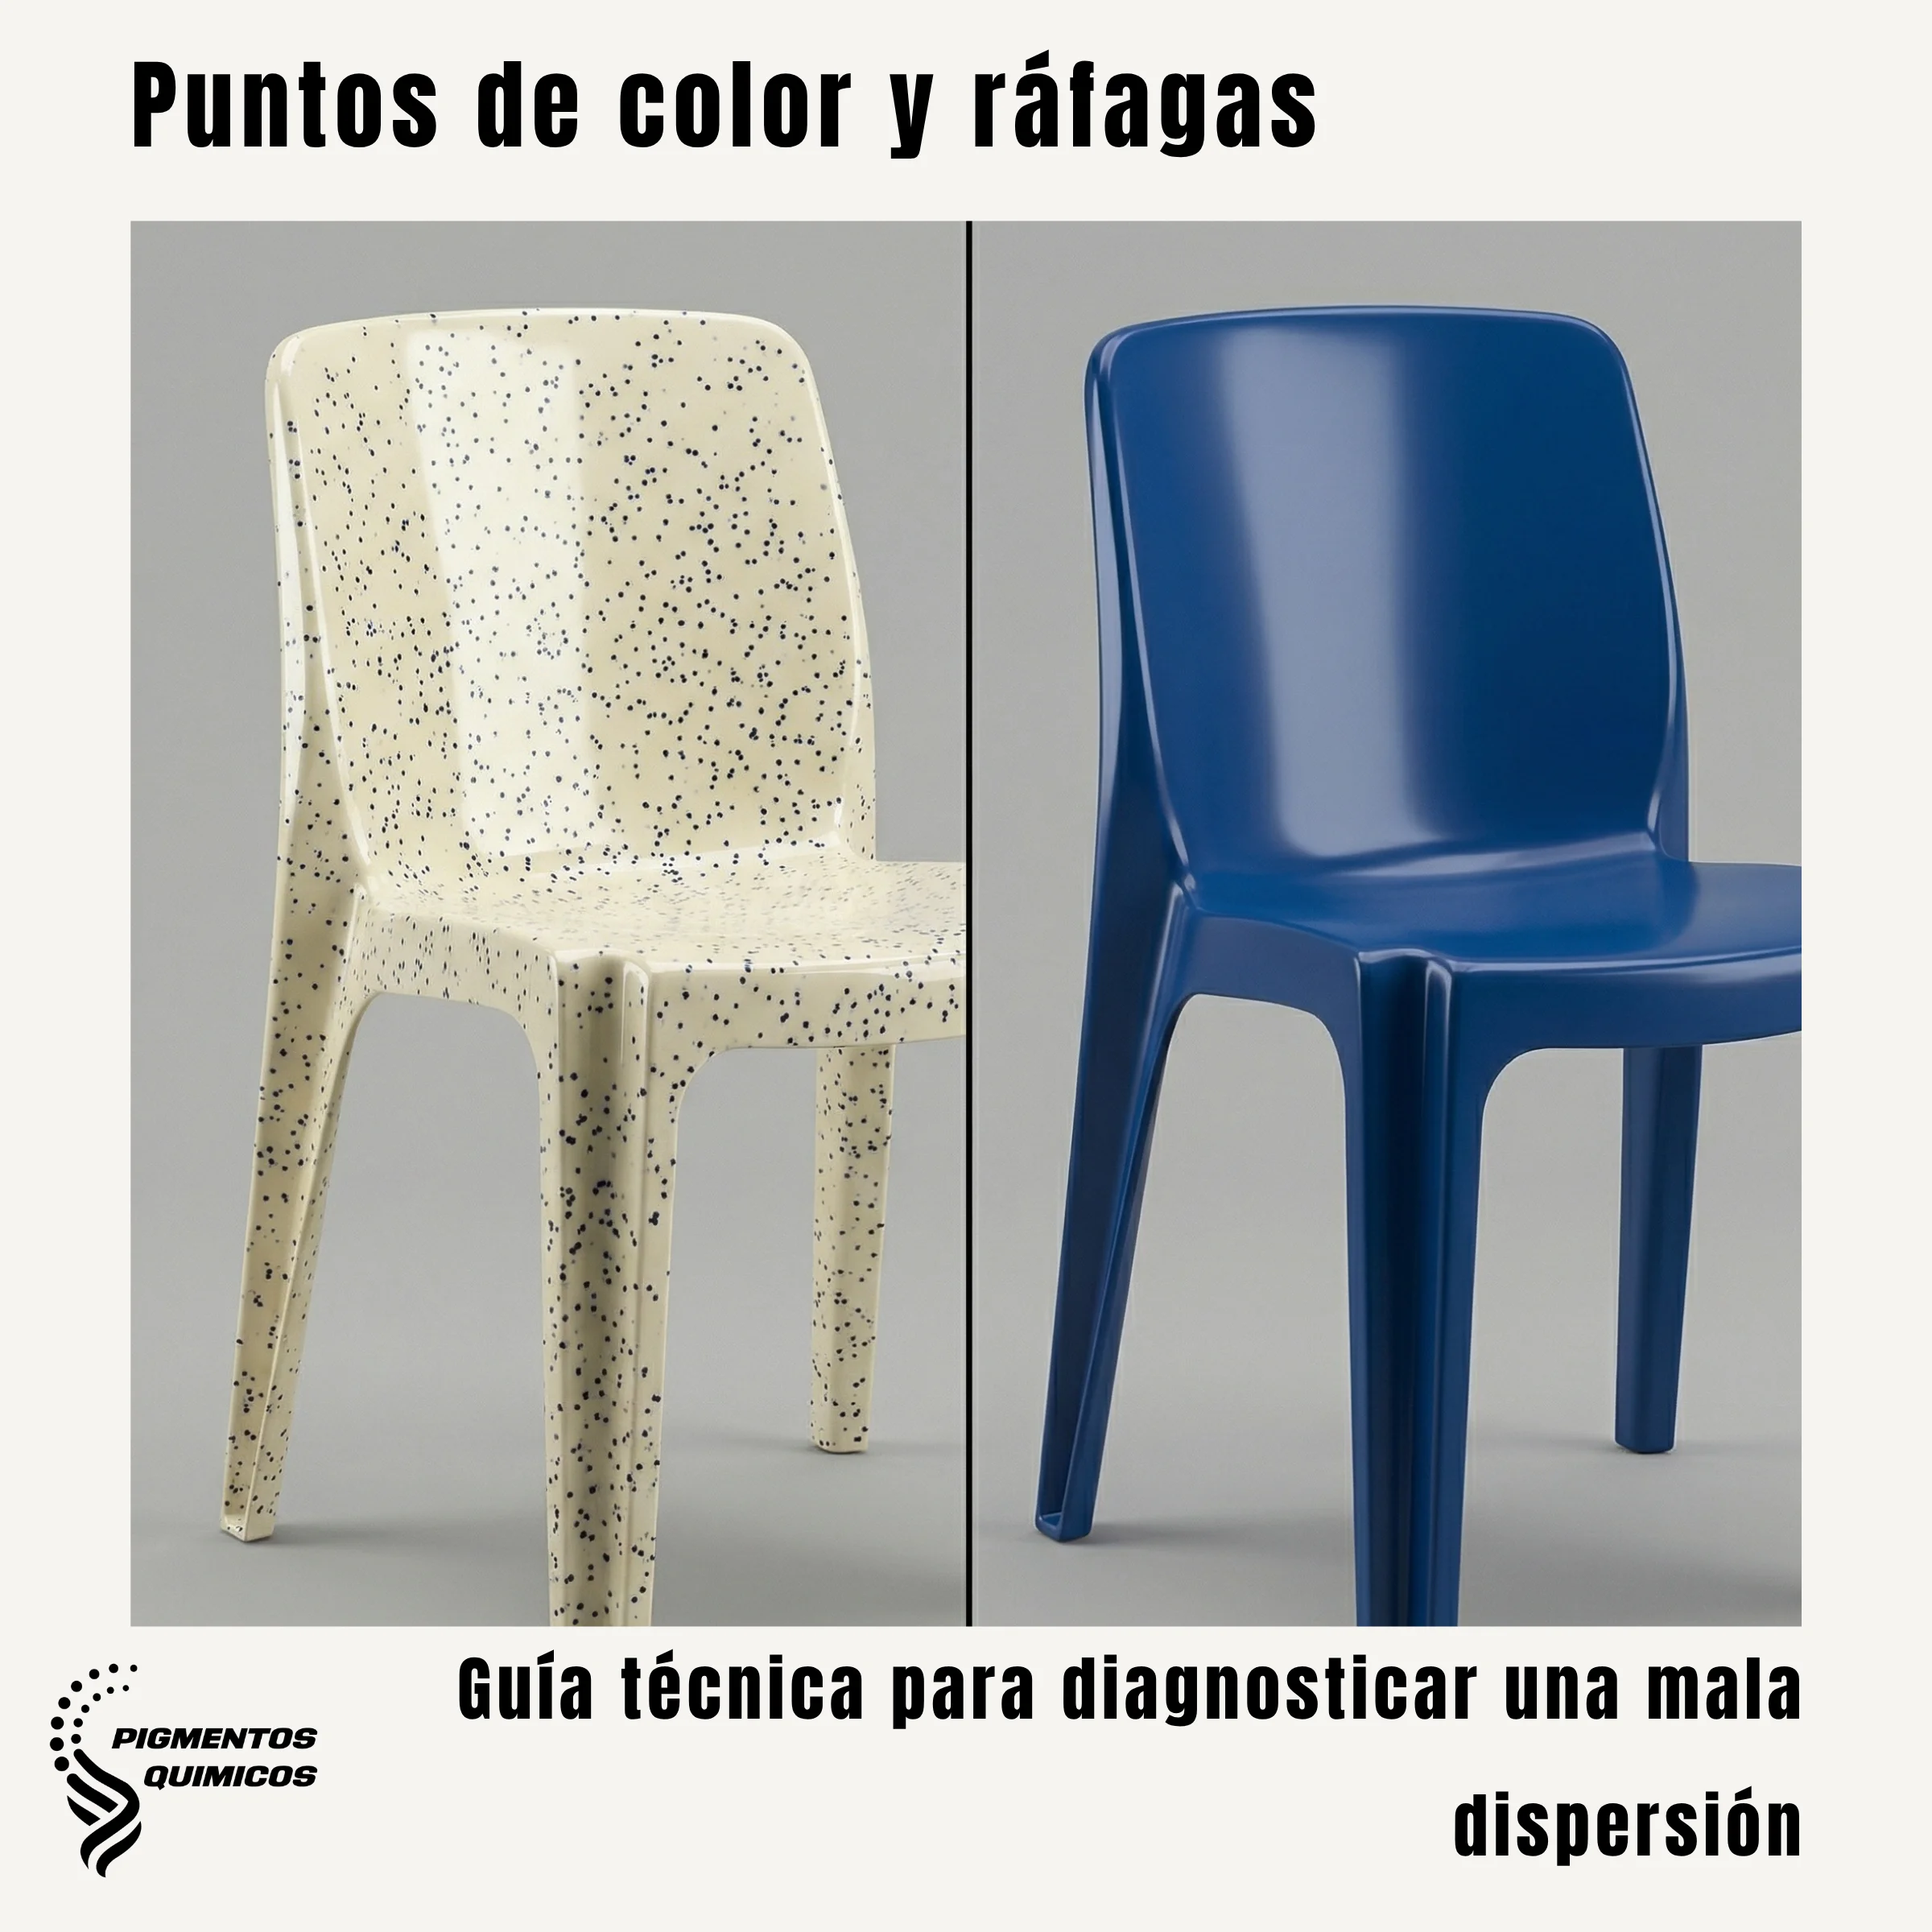
Color Spots and Streaks: Diagnosing Poor Dispersion in Plastic Production
Color spots and streaks are the most frequent dispersion defects. How to tell them apart and find the root cause in less than one production run.
In plastics processing, few problems are as costly and frustrating as part rejection due to visual defects. Color spots (non-dispersed pigments) and streaks (veining or marbling) not only affect aesthetics but can compromise the mechanical properties of the final product. Is the problem in the masterbatch, the resin, or the process? Learning to diagnose the source is the key to reducing scrap.
1. Color spots: the challenge of agglomerates
When small intense spots or 'granules' of color appear, we are facing a dispersion failure. This occurs when the pigments were not adequately separated during masterbatch manufacturing or failed to 'wet' and distribute in the processing machine.
2. Streaks and veining: distribution problems
Unlike spots, streaks or the marbling effect usually indicate poor distribution. The pigment is there, but it has not been uniformly mixed into the melt.
3. Plant diagnostic checklist
Before making drastic changes, check these three critical points:
4. The importance of technical compatibility
To avoid these defects, masterbatch selection must go beyond color. It is vital to ensure that the carrier (vehicle) of the concentrate is chemically and mechanically compatible with the final polymer. A masterbatch designed specifically for the process (injection, extrusion, blow molding) will drastically reduce machine adjustment time.
Frequently Asked Questions from the production technical department
How do I visually tell an agglomerate speck from a machine contamination speck?
If the speck has the color of the masterbatch being processed, more intense than the background of the part, it is probably a pigment agglomerate. If the speck is black regardless of the part color, it is probably carbonized material from the machine, residue from earlier production cycles or material degradation in dead zones of the system. If black specks appear with any masterbatch, the cause is the machine, not the masterbatch.
Which process adjustment should I try first when color specks appear?
The first adjustment is to increase screw back pressure by 20 to 30 percent, which raises shear energy during plasticizing and helps disperse agglomerates without raising process temperature. If more back pressure does not reduce the specks, the second adjustment is to review the screw temperature profile to verify the masterbatch melts properly before the mixing zone. Only if both adjustments fail should a change in masterbatch formulation be evaluated.
Do color streaks in injection molding always indicate a masterbatch problem?
Color streaks in injection molding can originate in the masterbatch, from a difference in MFI or melting temperature against the base resin, or in the mold design and filling conditions, turbulence zones, differential mold temperature or injection speed. Before attributing the defect to the masterbatch, check whether the streaks always appear in the same position on the part, which points to mold design or filling conditions, or in variable positions, which points to the material.
Related articles
Masterbatch Dosing: Correct Calculation for Color Consistency in Production
A dosing variation of 0.5% produces color differences visible to the naked eye. How to calculate and control it for lot-to-lot consistency.
5 Common Problems in Plastic Coloring and How to Solve Them
The five most frequent problems in plastic coloring: poor dispersion, thermal degradation, migration, batch inconsistency, and UV discoloration.
Metamerism in the Plastics Industry: The Invisible Phenomenon That Ruins Production Batches
Two parts with the same masterbatch look identical under plant lighting and different under daylight. That is metamerism, and it scraps entire batches.