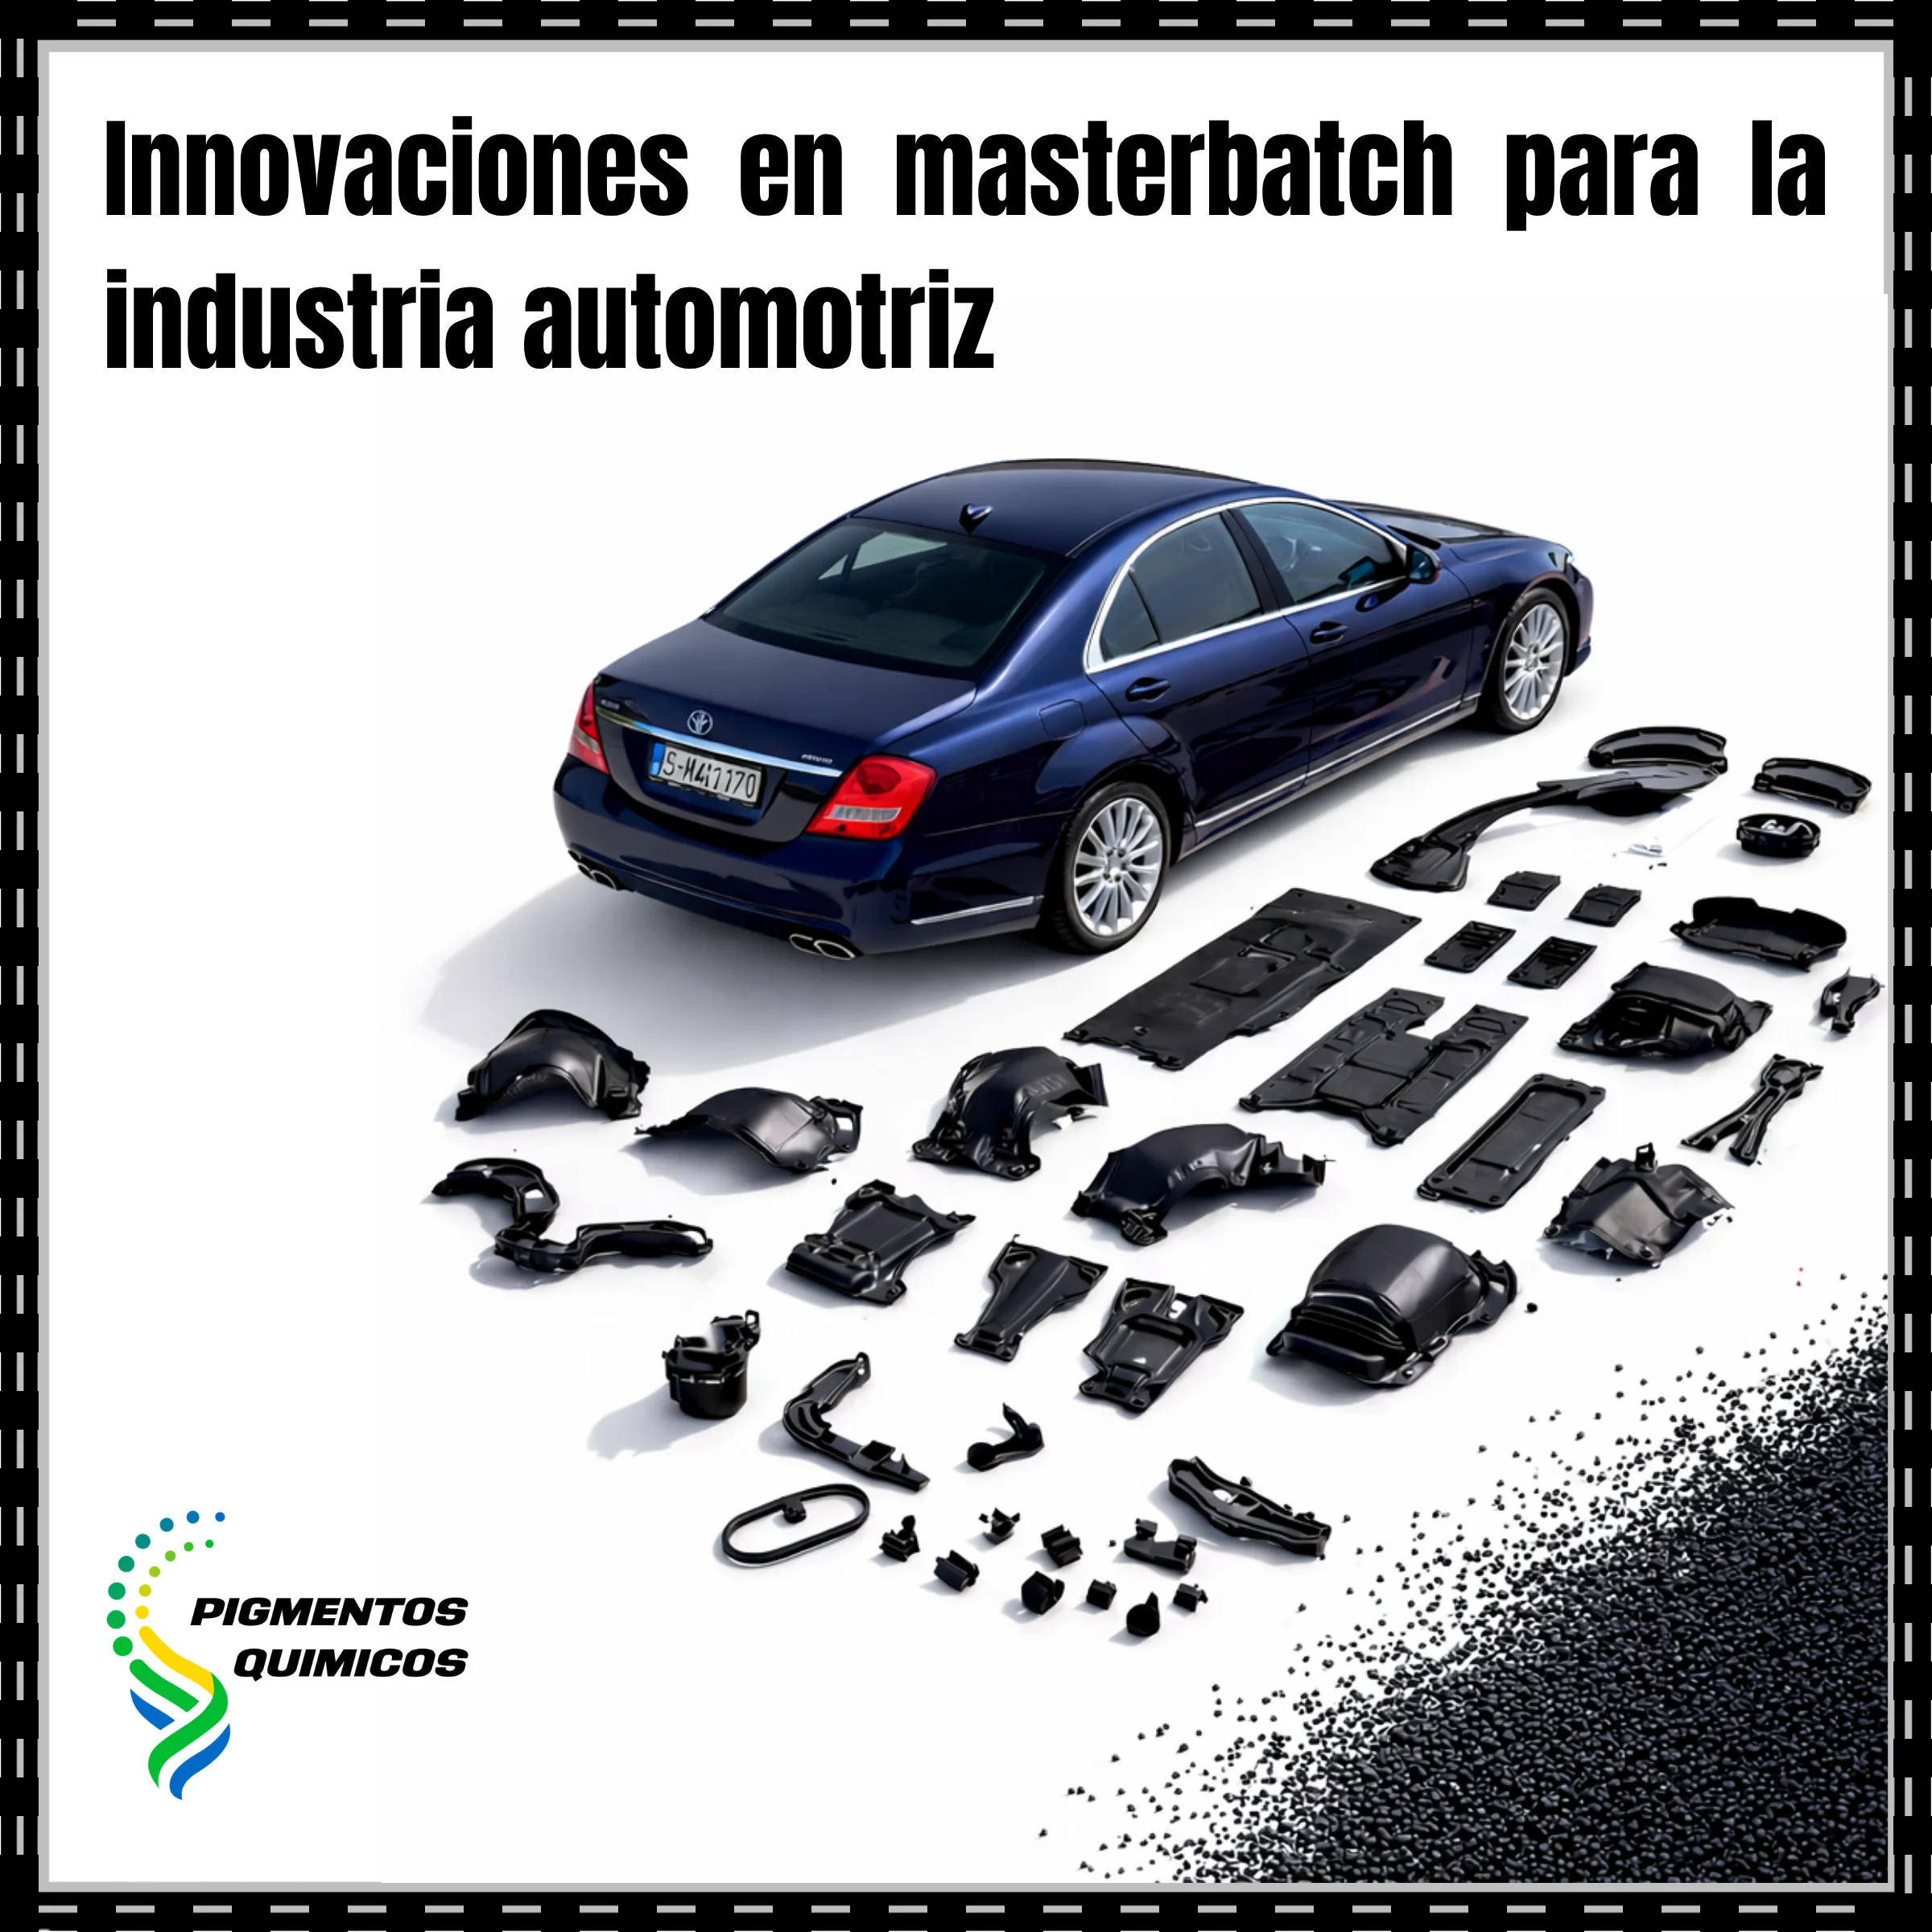
Masterbatch in the Automotive Industry: Technical Requirements the Generic Concentrate Cannot Meet
Automotive demands that color survive extreme thermal cycles, prolonged UV exposure, and decades of use. Generic masterbatch was not designed for that.
The automotive industry has some of the most demanding color and material specifications in plastics manufacturing. A bumper must match the paint on the adjacent steel panel under natural sunlight, in a tunnel, in a garage, and after 10 years of UV exposure. Generic masterbatch is not formulated for that environment.
What automotive OEMs require that standard masterbatch cannot deliver
The automotive supply chain sets material specifications at multiple levels: the OEM defines the color and performance requirements, Tier 1 suppliers must meet those requirements in finished components, and masterbatch suppliers must formulate to support both. Three technical areas separate automotive-grade masterbatch from general-purpose concentrates:
Interior applications: low-VOC and anti-migration requirements
Cabin components must comply with VOC emissions regulations that automotive standards set with increasingly strict criteria. Low-VOC masterbatch uses high-purity pigments with minimal residual volatile compounds, and carriers formulated with high-crystallinity polymers that reduce migration of volatile substances to the component surface. This requirement is critical for dashboards, door panels, and center consoles where VOC accumulation in the cabin directly impacts vehicle interior air quality.
Metallic and pearlescent finishes in automotive interiors require that effect pigments (aluminum, coated mica) do not migrate to adjacent surfaces during the vehicle's service life. Automotive effect masterbatch uses pigment encapsulation systems in high-viscosity carriers that fix metallic particle orientation and prevent migration under operating thermal cycles.
Qualification process in the automotive supply chain
Masterbatch approval in the automotive supply chain follows a specific qualification process: OEM pigment approval (some OEMs maintain approved pigment lists), masterbatch validation per the OEM's material standard (VDA standards in Europe, OEM-specific standards for Japanese and American manufacturers), and Tier 1 approval. Developing an automotive masterbatch from OEM color reference to first qualified sample takes 8–16 weeks and requires coordination between the color lab, the process technical team, and the supplier's quality organization.
Frequently Asked Questions from the technical departments of automotive suppliers
Which UV resistance standards should I specify in the masterbatch technical requirements?
The most common UV resistance standards in the automotive industry are SAE J1885 and ISO 105-B02, both xenon methods, for exterior components, and SAE J1960 for high performance applications. The specification must include the number of exposure hours, the evaluation illuminant, the pass criterion for color change, typically Delta E below 1.0 or below 1.5 under D65, and the acceptable rating scale for surface embrittlement.
Can a masterbatch be formulated to meet process fluid contact and UV resistance requirements at the same time?
The compatibility of a pigment with automotive process fluids, oils, coolants and brake fluids, and its UV resistance are independent properties that depend on pigment chemistry. Some high performance organic pigments, such as dioxazines and quinacridones, combine both properties. Specifying correctly requires defining both requirements from the start of the development so the formulation uses pigments that meet the two criteria simultaneously.
How long does it take to validate a color for an automotive component?
Validation time depends on the accelerated aging protocol the specification demands, since the exposure hours required by SAE J1885 or SAE J1960 cannot be shortened. Plan the color development around that test window rather than around the delivery date, and start it as soon as the target color and the exposure criterion are agreed.
Related articles
Masterbatch Dosing: Correct Calculation for Color Consistency in Production
A dosing variation of 0.5% produces color differences visible to the naked eye. How to calculate and control it for lot-to-lot consistency.
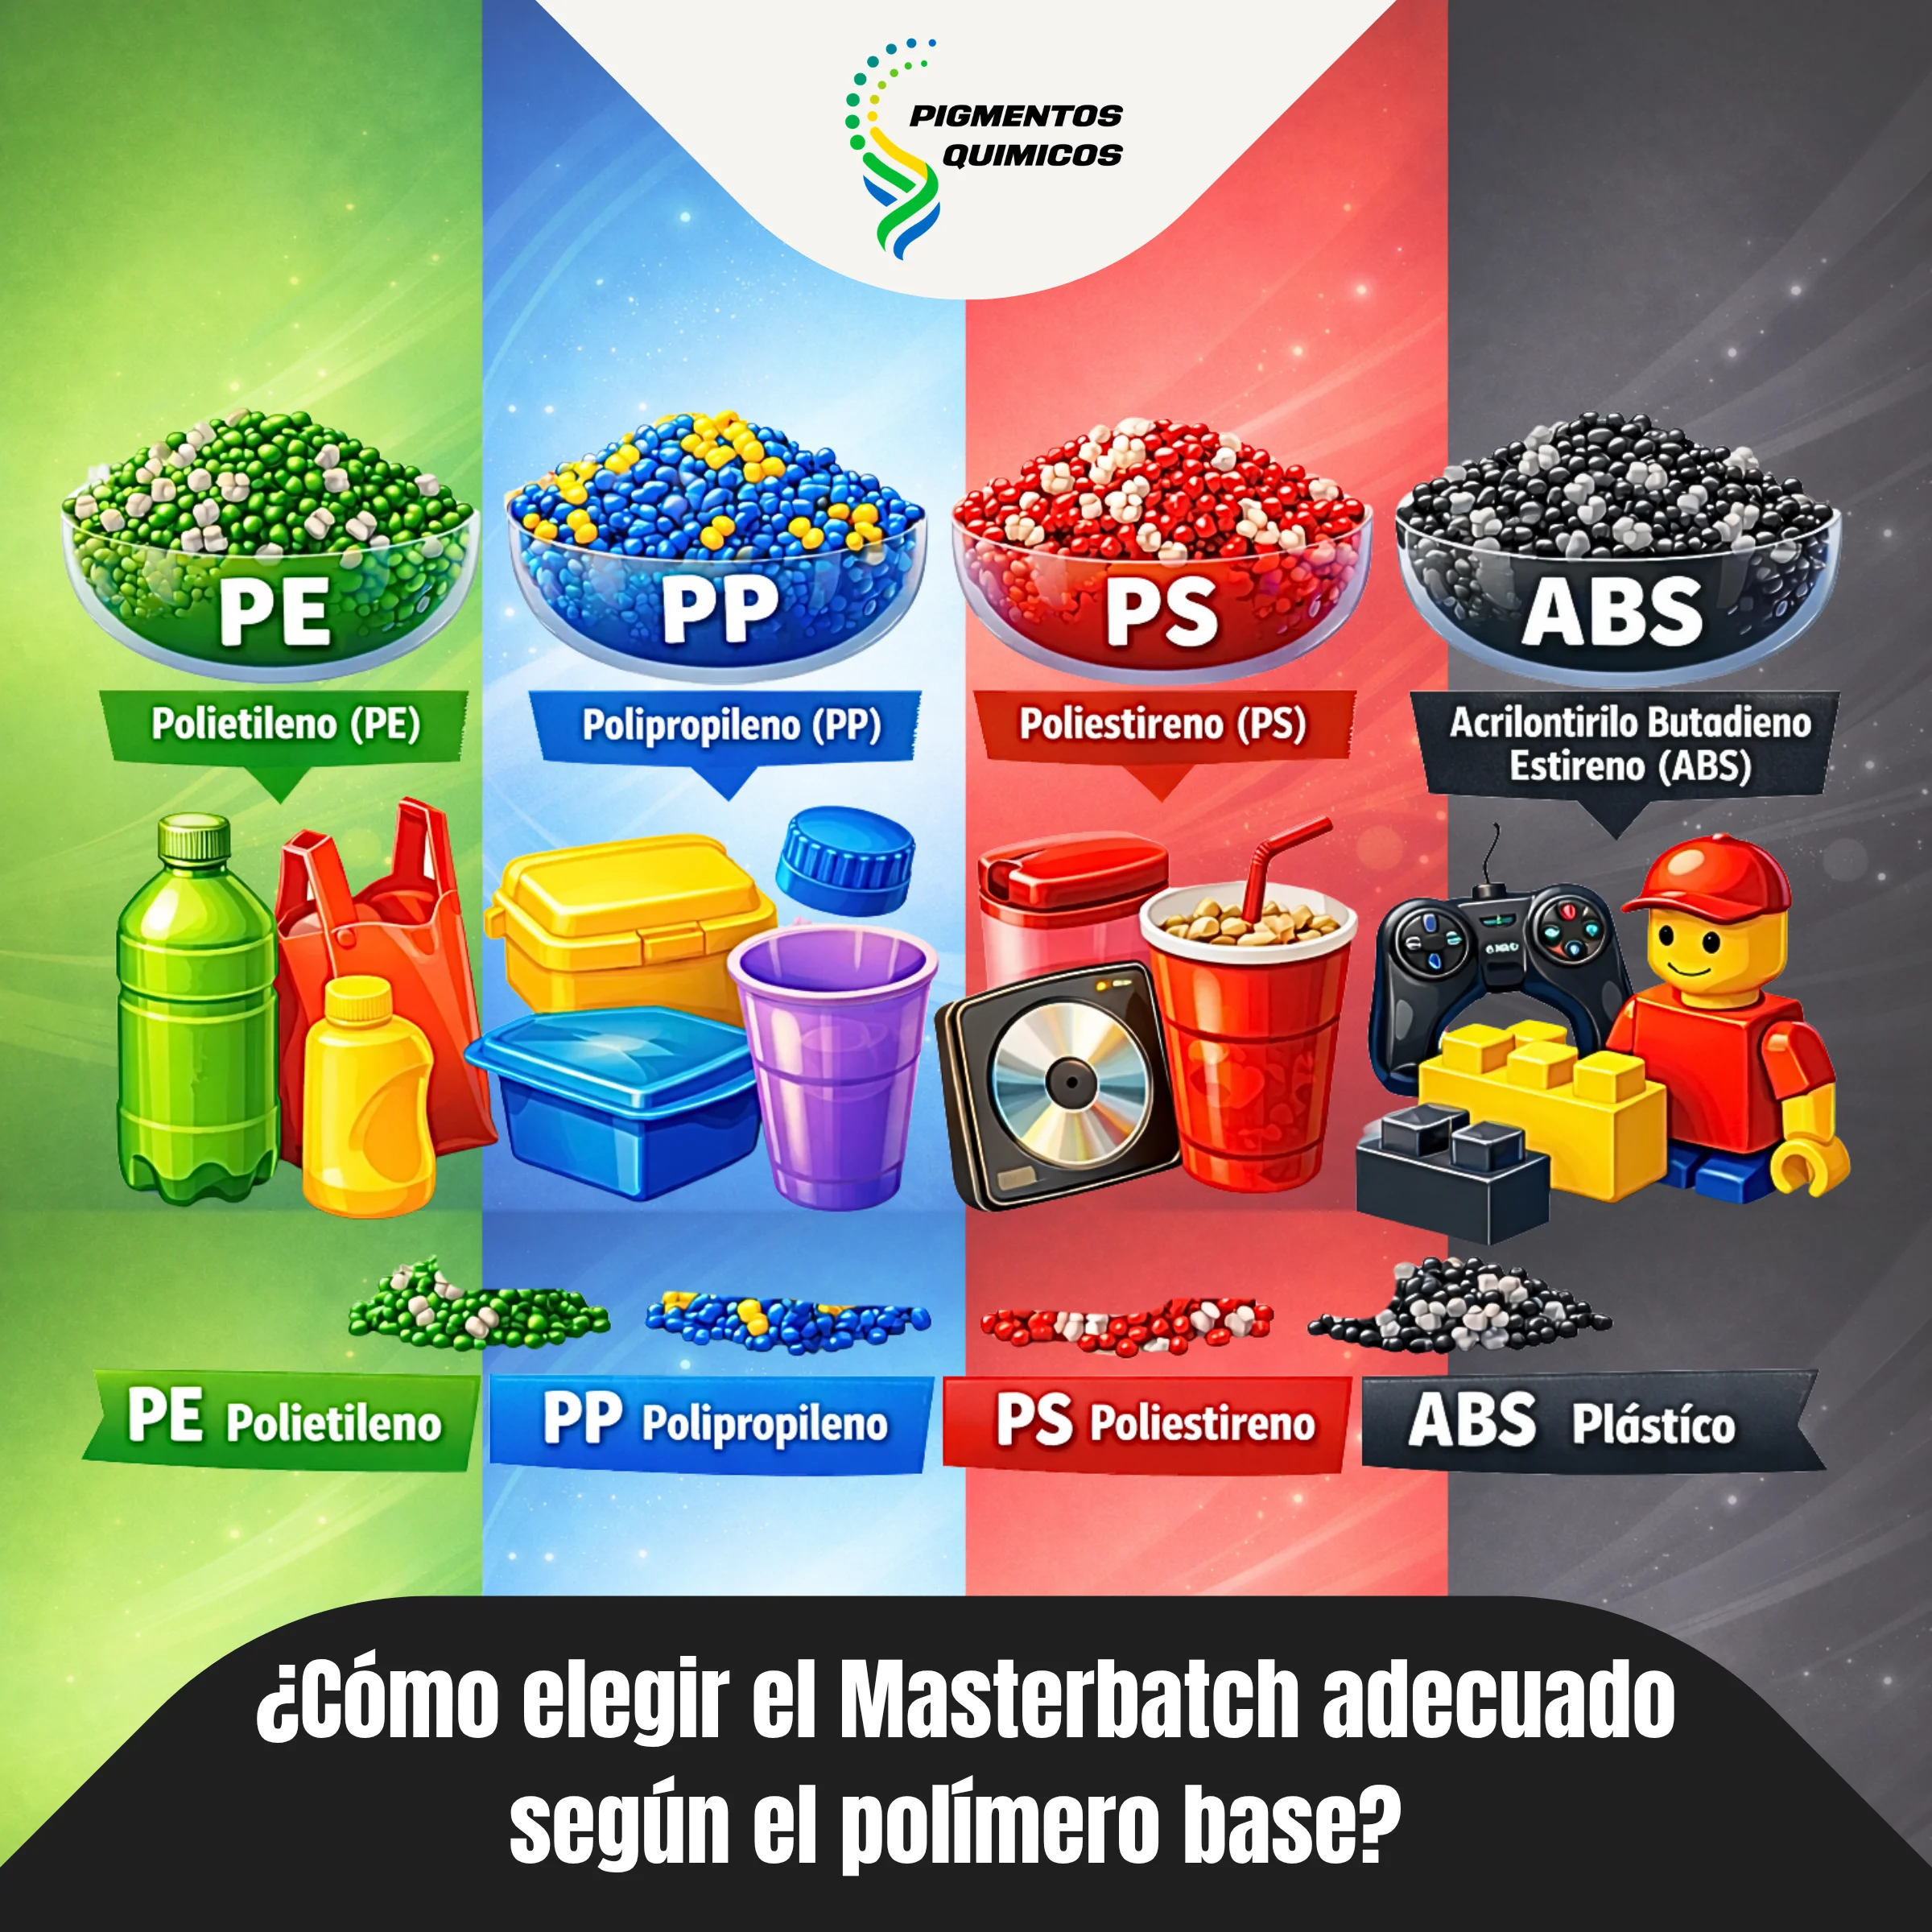
How to Choose the Right Masterbatch for Your Polymer: The Decision That Prevents Batch Failure
A masterbatch incompatible with the base polymer causes dispersion defects, mechanical loss, and rejections. The three parameters that define it.
Masterbatch vs. Liquid Pigments: Technical Analysis to Decide Correctly
Choosing between solid masterbatch and liquid pigment is not about unit price. Dosing stability, color consistency, and changeover cost decide the real cost.